
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








2026 Best PSC Tool Holder for CNC Machining?
Choosing the 2026 best Psc Tool Holder requires more than comparing catalog prices or polished product photos. A reliable choice must match the machine spindle, cutting conditions, tool geometry, and production goals. In CNC machining, the holder forms a critical link between spindle and cutter. Small errors can appear as vibration, poor surface finish, uneven tool wear, or unexpected dimensional drift.
Fit matters. Runout matters.
Dr. Scott Smith, a respected machining researcher, has expressed this practical principle: “The toolholder is part of the cutting system, not merely an accessory.” That view remains valuable when evaluating PSC designs. A capable holder should provide stable polygonal contact, consistent positioning, sufficient gripping force, and dependable coolant delivery. Operators should also inspect balancing quality, clamping repeatability, flange condition, and compatibility with the machine’s automatic tool changer.
Real shop-floor experience makes the decision less theoretical. A holder that performs well during a short aluminum test may behave differently during deep pocketing in hardened steel. Thermal growth, chips around the contact surfaces, and frequent tool changes can expose weaknesses quickly. Not every premium holder wins.
This guide compares leading PSC Tool Holder options for 2026 through measurable criteria, including radial runout, stiffness, tool-change reliability, maintenance demands, and total operating cost. Some conclusions may remain imperfect because machining results depend on the spindle, cutter, workpiece, and operator. That limitation deserves attention. The best holder is not always the most expensive model. It is the one that delivers repeatable performance under your actual cutting conditions.
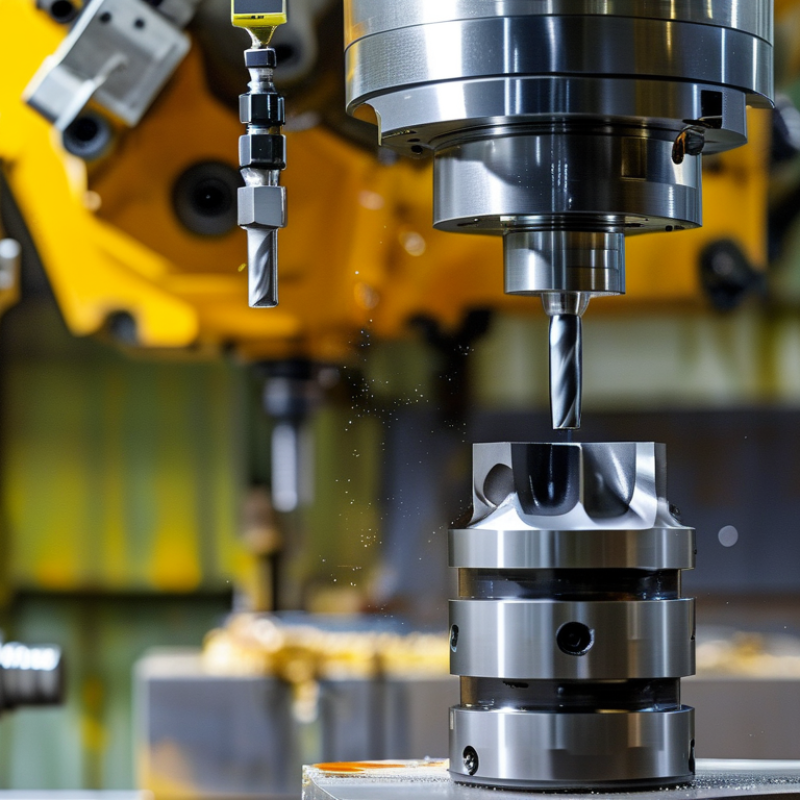
Table of Contents [Hide]
PSC Tool Holders Defined: ISO 26623 Geometry and Sizes 32–100
For 2026 CNC machining, the best PSC tool holder depends on fit, rigidity, and application. PSC means Polygonal Shank with a flange contact. ISO 26623 defines its geometry and dimensional relationships. Unlike a simple tapered connection, PSC uses polygonal faces to transfer torque and support radial stability. The flange also creates an axial reference surface. This combined contact can improve repeatability during heavy cutting and frequent tool changes.
Common ISO 26623 sizes include PSC 32, 40, 50, 63, 80, and 100. The number generally identifies the nominal shank size, not the cutting diameter. A PSC 63 holder may suit medium-to-heavy machining, while PSC 32 can fit smaller cutting systems. Always verify the spindle interface, gauge length, pull-stud design, and machine clearance. A correct size can still fail when the clamping system is mismatched.
In practical setup work, I check contact marks after test cuts. A clean, even pattern suggests proper seating. Uneven marks may indicate contamination, wear, or incorrect clamping force. Keep the polygonal surfaces clean. Tiny chips matter. Tool balance also deserves attention, especially above moderate spindle speeds. I once treated holder stiffness as the only priority, but excessive length caused vibration and poor surface finish. Shorter is often better, though not always. ISO geometry improves consistency, yet it cannot correct weak programming, poor workholding, or careless maintenance.