
- High-Performance Doors
-
- Applications
-
-
-
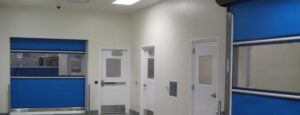
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








2026 Top Galvanized Steel Pipe for Water Suppliers?
Choosing the 2026 Top Galvanized Steel Pipe For Water Suppliers requires more than comparing prices. Water infrastructure demands traceable materials, stable coating quality, and reliable technical support. The right supplier should provide mill certificates, coating-thickness records, pressure data, and clear product standards. Small documents often reveal major differences.
Global steel capacity also shapes supplier reliability. The World Steel Association reported approximately 1.89 billion tonnes of crude steel production in 2023. This figure shows the scale of competition, but it does not guarantee water-grade performance. Buyers still need to verify manufacturing controls, zinc coating uniformity, dimensional tolerances, and corrosion testing. A polished factory may still provide incomplete evidence.
For potable-water projects, compliance must remain central. The World Health Organization’s Guidelines for Drinking-water Quality emphasizes protecting water safety from source to consumer. In North America, AWWA standards such as C651 support hygienic practices during water-main installation and disinfection. Suppliers should also explain how their Galvanized Steel Pipe For Water meets applicable regional requirements, including testing for coatings, fittings, and transported water quality.
Experience matters in the field. A pipe that survives warehouse handling may fail after repeated threading, cutting, or exposure to wet soil. That detail is easy to overlook. Installation photographs, third-party inspection reports, warranty terms, and references from municipal or industrial projects can strengthen supplier evaluation. Still, no ranking is permanent. Freight costs, zinc prices, energy conditions, and certification updates may change the 2026 market quickly. This guide therefore focuses on verifiable performance, not attractive claims alone.
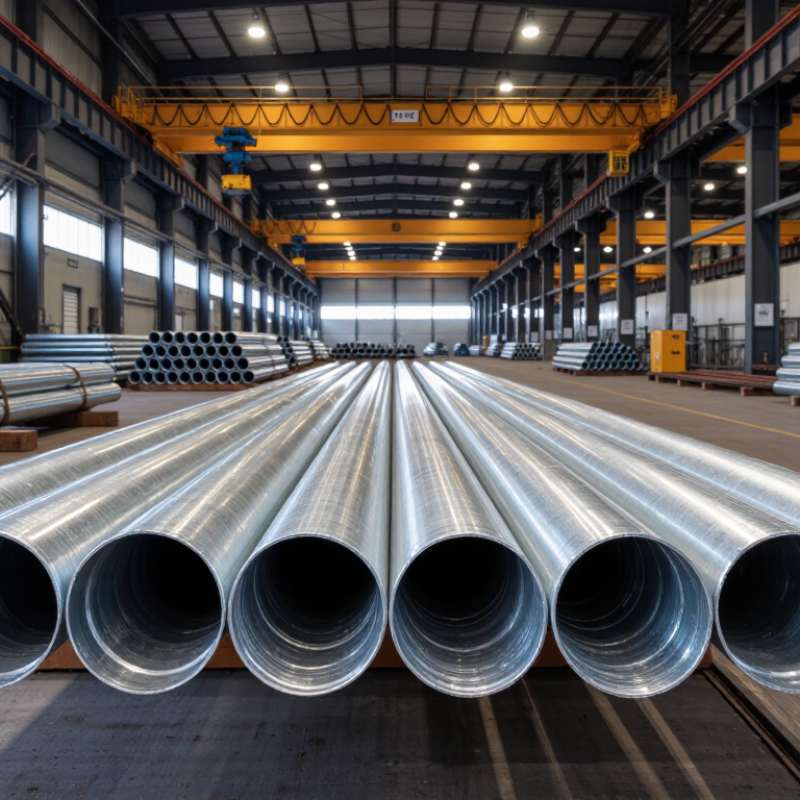
Table of Contents [Hide]
Definition and Uses of Galvanized Steel Pipes for Water Systems
Galvanized steel pipe is carbon steel protected by a bonded zinc coating. The zinc barrier slows rust and gives the pipe a durable, metallic surface. This pipe is commonly used for cold-water distribution, outdoor service lines, irrigation, and utility connections. Its familiar silver-gray finish makes damage easier to notice during installation.
For 2026 water projects, reliable suppliers should provide clear information about coating thickness, pipe dimensions, pressure ratings, and production tests. Traceable inspection records matter. So does technical support. Suppliers should ask about water chemistry, operating temperature, connection methods, and local installation requirements. A low price alone is not enough. It may hide weak coating control or inconsistent wall thickness.
Field inspections often find damaged zinc around cut threads and fittings. Those areas need proper protection before the system is placed into service. Galvanized pipe should also be cleaned, flushed, and checked for debris after installation. One practical concern remains. Internal corrosion can reduce the passage over time, especially in aggressive water. Hot-water use may accelerate zinc deterioration. I would not specify this material automatically for every project. That judgment can be imperfect. A careful engineer compares water quality, service life, maintenance access, and approved alternatives before selecting a supplier or pipe system.