
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








2026 Top Nylon Flat Transmission Belt Manufacturers?
The 2026 market for Nylon Flat Transmission Belt products is becoming more demanding. Buyers now assess more than price, width, and tensile strength. They examine material consistency, splice quality, tracking stability, noise control, and service support. A belt that looks strong in a catalog may still fail under heat, dust, or repeated shock loads.
Dr. Robert C. Budynas, a mechanical power-transmission specialist, once stated, “Reliable machine performance begins with correct component selection.” This principle matters when comparing leading Nylon Flat Transmission Belt manufacturers. The strongest suppliers usually combine controlled nylon fabric, accurate coating systems, dependable joining methods, and documented testing. They also explain operating limits clearly. That transparency matters.
Small details often decide performance.
This guide examines manufacturers expected to influence the 2026 market. It considers production capability, technical expertise, customization, quality assurance, delivery reliability, and after-sales support. Real factory experience may differ from promotional claims. That deserves attention. A supplier with advanced machinery may still struggle with regional service or replacement availability. Another manufacturer may offer modest branding but deliver consistent belts for years.
The ranking should not be treated as absolute. Application conditions vary widely. A belt used on a packaging line faces different demands from one used in textile machinery or paper processing. Readers should verify test data, installation guidance, and warranty terms before making a final decision. This comparison aims to support careful evaluation, not replace engineering judgment.
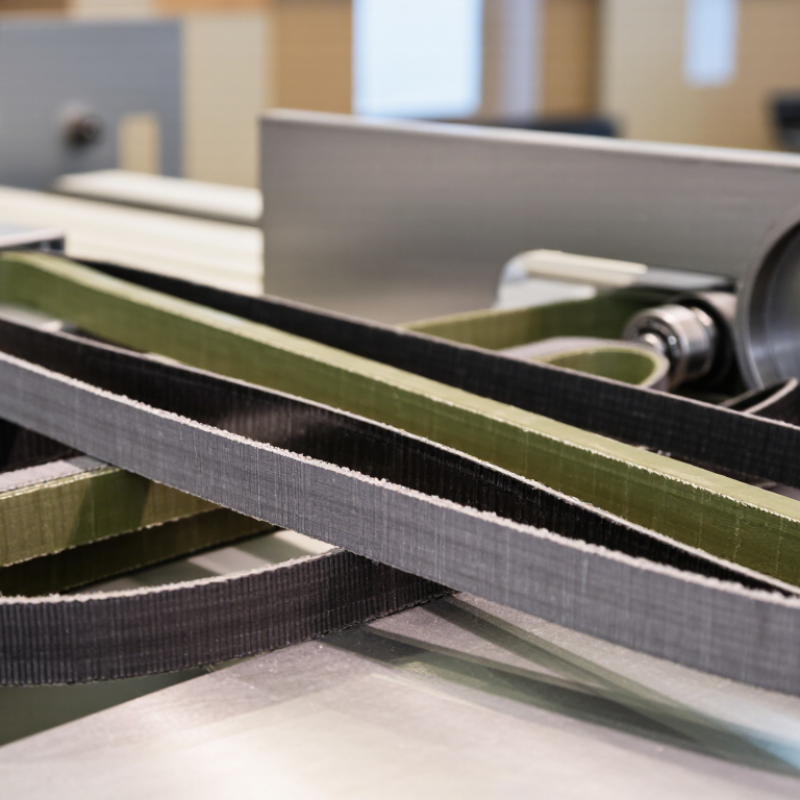
Table of Contents [Hide]
Nylon Flat Transmission Belts: Definition, Structure, and Operating Principles
In 2026, top nylon flat transmission belt manufacturers should prove more than production capacity. A nylon flat transmission belt transfers power between pulleys through surface friction. It is commonly used in conveyors, packaging machines, textile equipment, and light industrial drives. The belt looks simple. Its design is not.
The main structure includes a strong nylon tensile layer and one or more protective covers. The nylon layer carries tension and limits stretching. The cover improves grip, wear resistance, and flexibility. Some belts use polyurethane, PVC, rubber, or fabric coatings, depending on speed and load.
During operation, a driving pulley pulls the belt forward. Friction then moves the belt and driven pulley together. Correct tension matters. Too little causes slipping and heat. Too much increases bearing loads and belt fatigue. Pulley alignment also affects tracking, even when the belt appears properly installed.
Tips: Ask manufacturers for tensile data, cover hardness, joint methods, and operating temperature ranges. Check whether the belt suits oil, moisture, dust, and repeated bending. Measure pulley diameter carefully. A small error can shorten service life. In maintenance work, I have seen clean belts fail because tension was guessed. That mistake is easy to repeat. Real installations are rarely perfect, so inspection access and adjustment design deserve attention. A reliable supplier should explain testing methods, tolerances, and quality records without hiding behind vague claims.