
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








China Best CNC Multifunctional Side Hole Drill Supplier
Choosing the China Best CNC Multifunctional Side Hole Drill Supplier requires more than comparing catalog prices. This equipment must deliver accurate side drilling, stable feeding, clean edges, and repeatable performance during demanding production. A reliable supplier should explain spindle power, drilling diameter, workpiece thickness, servo control, dust protection, and after-sales support clearly. Vague promises are warning signs.
David Lin, a CNC manufacturing consultant with more than 20 years of workshop experience, says, “A good machine is not judged by its brochure; it is judged by the hole repeated after thousands of cycles.” His view reflects a practical truth. A CNC Multifunctional Side Hole Drill may appear advanced, yet poor calibration can create uneven holes, tool vibration, or fitting problems during assembly. Small errors become expensive quickly.
This guide examines how Chinese manufacturers design, test, and support the CNC Multifunctional Side Hole Drill. It considers frame rigidity, drilling accuracy, automatic positioning, software usability, component quality, and production testing. Factory videos help, but they are not enough. Ask for sample results, maintenance records, electrical standards, and clear warranty terms. Speak with technical staff, not only sales representatives.
No supplier is perfect. Some factories offer strong engineering but weaker documentation. Others provide attractive prices but limited training. That deserves reflection. The best decision balances machine performance, communication, service response, and long-term operating cost. Buyers should inspect details closely, because reliability is built through evidence, not confident language.
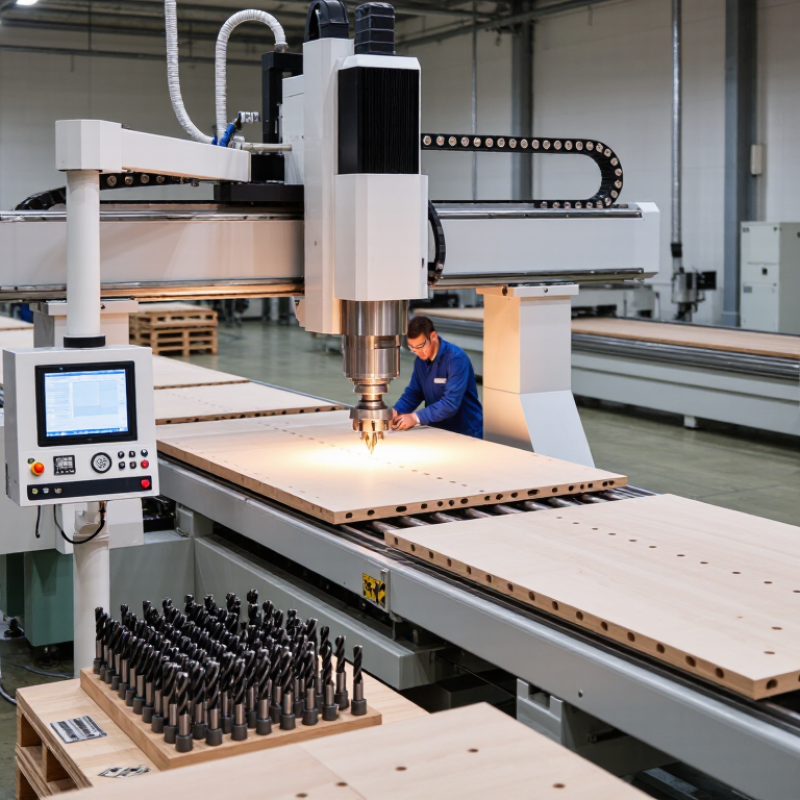
Table of Contents [Hide]
Definition and Core Functions of a CNC Multifunctional Side Hole Drill
A CNC multifunctional side hole drill is a computer-controlled machine for horizontal drilling on panels, frames, and engineered boards. It follows programmed coordinates, clamps the workpiece, and drives a spindle through the material. Its main value is repeatable side-hole positioning.
Depending on configuration, it can drill, mill grooves, and create dowel or connector holes in one setup. This reduces manual marking and limits handling errors. The operator usually imports a CAD file, selects tool parameters, and checks the first piece. Grand View Research reported a projected 9.5% CAGR for the global CNC machine market from 2023 to 2030. That growth reflects demand for flexible, automated production, not just faster drilling.
Tips: Confirm panel thickness before programming. Use sharp tools and stable clamping. Test one sample first. Measure hole depth manually. It is not a magic box. Dust buildup, poor calibration, or incorrect coordinates can still damage a panel. A useful improvement is adding barcode-based job identification, although this requires disciplined data management. Industry 4.0 reports from McKinsey also link connected machines with better production visibility, but actual gains depend on maintenance habits and operator training.