
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








China Best Blind Flanges Manufacturer and Supplier?
Choosing the China Best Blind Flanges Manufacturer and Supplier requires more than comparing prices. It requires evidence.
The global industrial valves market continues to expand, according to Grand View Research. Its industry report identifies infrastructure investment, energy projects, and process manufacturing as major growth drivers. These sectors also create steady demand for reliable Blind Flanges. However, market growth does not guarantee supplier quality.
A serious manufacturer should demonstrate material traceability, dimensional control, and pressure-testing records. Look for certificates covering ASTM, ASME, EN, or equivalent requirements. Request heat numbers, inspection reports, and clear tolerances. A flange may appear perfect on a warehouse shelf. Its performance depends on machining accuracy, steel chemistry, gasket contact, and installation torque.
John H. Bickford, a recognized authority on bolted-joint engineering, wrote, “The purpose of a bolt is to produce and maintain clamping force.” That principle matters here. Poor bolt loading can undermine an excellent flange.
Small details matter.
A dependable Chinese supplier should explain forging routes, ultrasonic testing, coating options, and export packaging. Wooden crates, sealed flange faces, and visible identification labels are practical signs of control. Site audits and independent inspections add confidence.
Yet no supplier is automatically perfect. Some websites show impressive certificates but provide weak technical responses. That deserves scrutiny. A careful buyer should compare production capacity, inspection depth, delivery history, and after-sales communication.
This guide examines leading China Blind Flanges manufacturers and suppliers through those practical standards. The goal is not the cheapest quotation. It is a traceable, correctly engineered product that performs when the pipeline is finally pressurized.
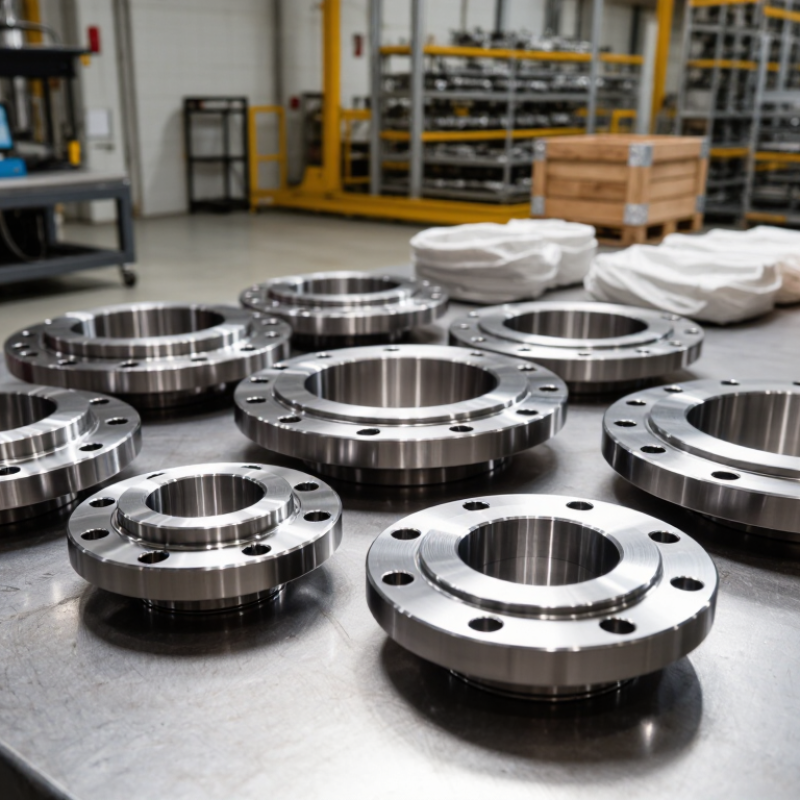
Table of Contents [Hide]
What Are Blind Flanges and Where Are They Used?
A blind flange is a solid, flat-ended flange used to close a pipe, nozzle, or vessel opening. Unlike a weld neck or slip-on flange, it has no bore. Its raised face compresses a gasket against the matching flange, while bolts create the sealing force.
Blind flanges are common at pipeline ends, pump outlets, pressure vessels, and inspection points. Operators use them during hydrostatic testing, maintenance, or future line extensions. They can isolate equipment without removing long pipe sections. The metal disc looks simple, but pressure rating, material grade, and facing details must match the system. A small mismatch can cause leakage.
In field inspections, technicians check the flange face for scratches, rust, and uneven wear. They also confirm bolt length, gasket type, and tightening sequence. The wrong gasket may fail even when the flange is correctly machined. This detail is sometimes overlooked. For high-pressure service, dimensional standards, heat treatment records, and test reports should be reviewed before shipment. A reliable Chinese manufacturer or supplier should provide traceable material certificates and clear inspection data. However, paperwork alone is not enough; random dimensional checks and visual inspection still matter. The flange may pass a factory check and fail after poor installation.