
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








Best Stainless Steel Coil Manufacturer in China?
Choosing the Best Stainless Steel Coil Manufacturer in China requires more than comparing price lists. Buyers must examine metallurgy, traceability, delivery performance, and verified production controls. The International Stainless Steel Forum reported global crude stainless steel production of approximately 58.4 million tonnes in 2023. That scale shows strong demand, but it also makes supplier selection more complex.
Look closely.
A capable Stainless Steel Coil Manufacturer should provide mill test certificates, heat numbers, surface inspection records, and clear thickness tolerances. These documents help confirm whether the coil matches standards such as ASTM A240 or EN 10088. Practical details matter too. A 2B-finished 304 coil should arrive with consistent brightness, protected edges, and packaging that prevents moisture damage during sea transport. The World Steel Association continues to identify construction, automotive, and manufacturing as major steel-consuming sectors, supporting the need for stable stainless supply chains.
However, published capacity is not proof of dependable performance. Factory audits, sample testing, and customer references reveal more than polished websites. Reliable manufacturers should explain their annealing process, slitting accuracy, minimum order quantities, and response procedures for nonconforming material. Certification helps.
It is also wise to question perfect claims. Some suppliers may show impressive equipment but provide limited evidence of export experience or batch consistency. A careful review should compare production records, inspection methods, lead times, and after-sales accountability. This guide evaluates those factors using industry references and practical purchasing experience, while recognizing that no supplier is ideal for every application.
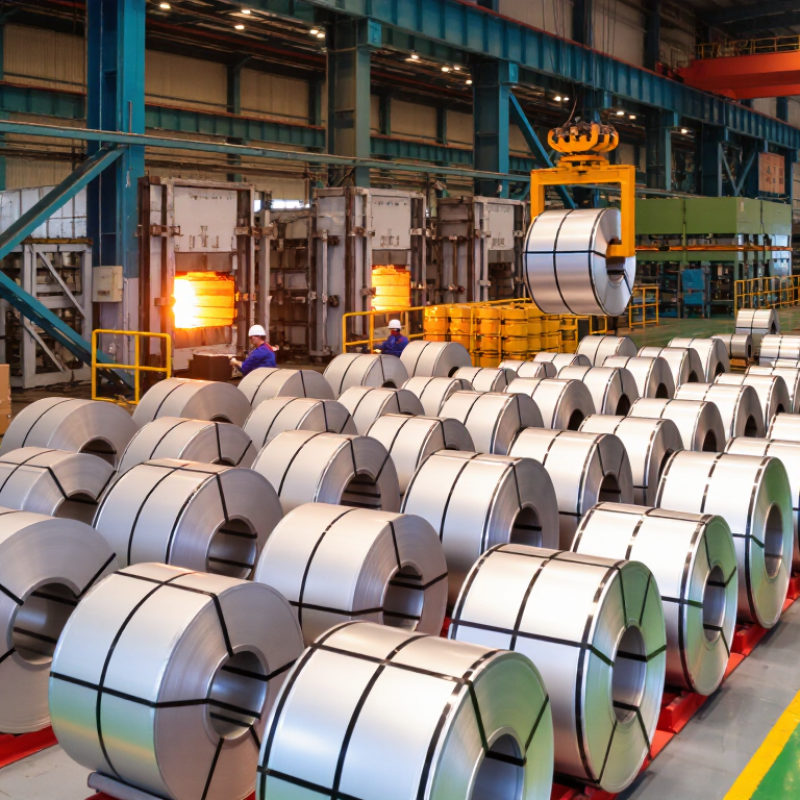
Table of Contents [Hide]
What Makes a Stainless Steel Coil Manufacturer the Best in China
Best Stainless Steel Coil Manufacturer in China?
What Makes a Stainless Steel Coil Manufacturer the Best in China
The best manufacturer is not defined by a low quotation alone. It combines stable production, accurate documentation, and practical communication. Experienced buyers inspect how a mill controls chemistry, thickness, width, and surface finish. A reliable producer records each coil by heat number, production date, and inspection result. Small details matter.
Technical capability should be visible in the factory process. Modern rolling equipment helps maintain tight thickness tolerances across long coils. Annealing and pickling must be controlled carefully, especially for demanding corrosion-resistant applications. Independent testing can verify tensile strength, hardness, elongation, and chemical composition. Standards such as ASTM, EN, or JIS should match the buyer’s drawings and service conditions. A certificate is useful, but traceable test data is stronger.
Quality also includes packing and delivery discipline. Coils need firm strapping, moisture protection, clear labels, and loading plans suited to sea transport. During supplier evaluations, buyers should compare rejected-coil rates, corrective-action records, and response times. No mill gets every decision right. The difference appears in how openly it investigates a surface mark or dimensional complaint. Some suppliers promise everything too quickly. That deserves caution. A dependable manufacturer explains limits, suggests workable grades, and provides samples before large production. Regular factory audits, video inspections, and pre-shipment checks can expose gaps that polished sales materials hide.