
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








China Top Metal Irregular Nozzle Manufacturers?
Choosing China’s top Metal Irregular Nozzle manufacturers requires more than comparing product photos. These components often serve custom spraying, cooling, mixing, or dosing systems. Their unusual geometry can affect flow direction, pressure loss, sealing, and maintenance. A reliable manufacturer should explain material selection, machining limits, surface finish, and application suitability. Stainless steel, brass, aluminum, and engineered alloys may perform differently in heat, corrosion, and abrasive environments. Small details matter. Thread accuracy matters. So does repeatability between batches.
This guide examines manufacturers through practical evidence, not marketing language. It considers engineering experience, drawing review, prototype support, inspection records, and communication during production. Useful checks include dimensional reports, flow testing, pressure testing where appropriate, and traceable material documentation. ISO certifications can support confidence, but they should not replace factory verification. A polished website is not proof. Samples may look excellent while production consistency remains uncertain. That is where buyers need careful questions and realistic expectations. No supplier is perfect. Even experienced teams can miss a tolerance or misunderstand an installation angle. Clear drawings, approved samples, and written acceptance criteria reduce that risk. The strongest candidates usually show stable processes, responsive technical support, and transparent limits. This comparison aims to help engineers and purchasing teams identify capable Chinese suppliers for dependable metal irregular nozzles, while recognizing that final selection must match actual working conditions.
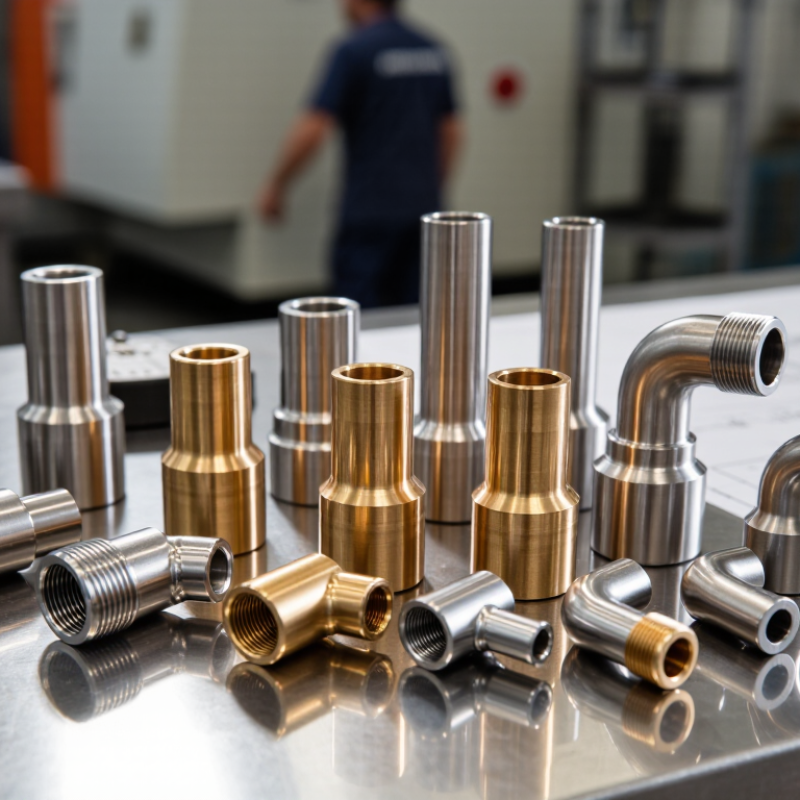
Table of Contents [Hide]
What Are Metal Irregular Nozzles and Where Are They Used?
China Top Metal Irregular Nozzle Manufacturers?
Metal irregular nozzles are engineered outlets with non-circular openings or uneven internal channels. Common designs include fan, slot, annular, multi-port, and elliptical patterns. Stainless steel, nickel alloys, brass, and titanium are selected according to temperature, corrosion, and pressure. The geometry controls spray angle, droplet size, impact force, and coverage. The term is not perfectly standardized. That gap matters.
These nozzles appear in spray drying, industrial washing, surface coating, combustion systems, food processing, and water treatment. A slot nozzle can create a wide, thin curtain across moving sheets. A multi-port nozzle can distribute cleaning fluid around complex equipment.
Grand View Research valued the global spray drying equipment market at roughly USD 5 billion in 2023 showing why precise atomization remains commercially important. Yet this figure covers equipment, not irregular nozzles alone.
China-based manufacturers commonly produce these parts through CNC machining, EDM, laser welding, and metal additive manufacturing. The Wohlers Report 2024 estimated the additive manufacturing industry reached USD 20.035 billion in 2023, supporting more complex flow-channel designs.
Reliable suppliers should provide material certificates, dimensional inspection, pressure testing, and measured flow-rate data. Engineers should also request spray-pattern tests at actual operating pressure. A drawing alone is insufficient.
In practice, I would question any supplier promising perfect uniformity without test conditions, because viscosity, temperature, and installation angle can change performance.