
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








China Top Custom Zinc Alloy Die Casting Supplier
China has become a major manufacturing base for precision metal components. Within this market, Custom Zinc Alloy Die Casting supports products that need detailed shapes, stable dimensions, and attractive surfaces. Typical applications include door hardware, lighting parts, furniture fittings, automotive accessories, and electronic housings.
A professional supplier should understand the complete casting process. This includes alloy selection, mold design, die temperature, injection pressure, trimming, polishing, plating, and inspection. Small details matter. A sharp logo, thin wall, or hidden screw boss can affect production results. Experienced engineers usually review 3D drawings before tooling begins. They may also suggest draft angles, stronger ribs, or improved gate locations. These changes can reduce porosity and protect long-term performance.
Quality needs evidence.
Reliable factories should provide material details, dimensional reports, sample approval records, and traceable production information. Surface finishes may include chrome, nickel, powder coating, painting, or brushed effects. Each finish should be tested against the product’s working environment. Salt spray performance, coating adhesion, and wear resistance cannot be judged by appearance alone. A bright sample can still hide weak plating.
No supplier is perfect. Even experienced teams can miss a difficult tolerance or underestimate a finishing problem. That is why clear communication, prototype testing, and corrective action are essential. Buyers should review equipment, inspection methods, production capacity, and export experience before placing large orders. A dependable China Custom Zinc Alloy Die Casting supplier does more than quote a low price. It offers practical engineering support, consistent manufacturing, and honest feedback when a design needs improvement. That balance builds trust over time.
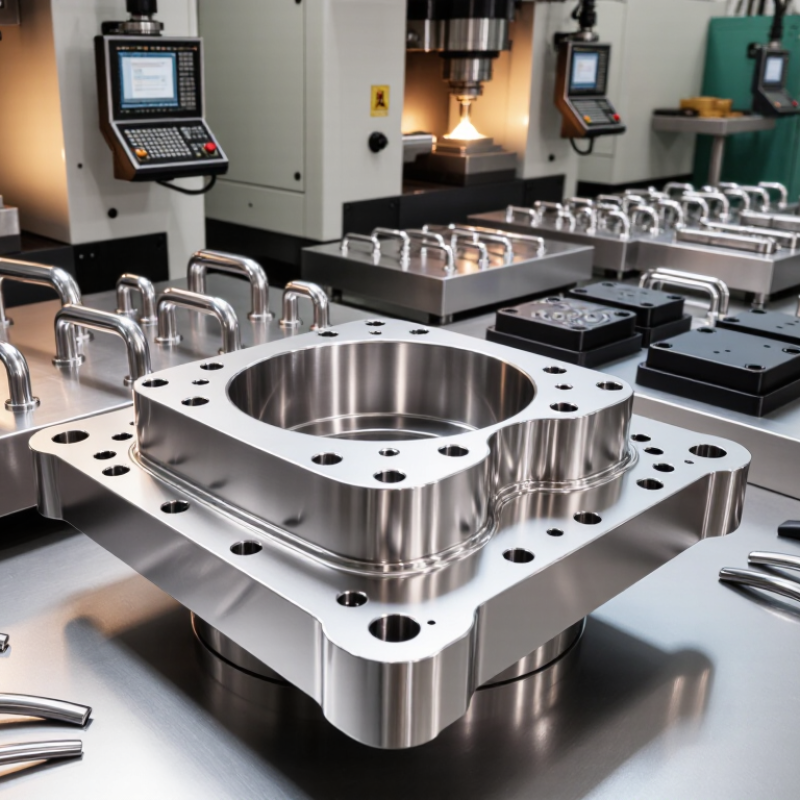
Table of Contents [Hide]
Definition and Role of Custom Zinc Alloy Die Casting
China Top Custom Zinc Alloy Die Casting Supplier
Definition and Role of Custom Zinc Alloy Die Casting
Custom zinc alloy die casting is a manufacturing process that injects molten zinc into a precision steel mold under high pressure. The mold creates the required geometry repeatedly, including thin walls, ribs, threads, and small mounting features. It is more than shape. The process can reduce machining, improve surface consistency, and support efficient production of hardware, housings, handles, and industrial components.
A capable supplier treats customization as an engineering task, not just a mold-making service. Engineers review the 3D model, wall thickness, draft angles, gate locations, and expected loads before production. They may recommend an alloy change when strength, corrosion resistance, or operating temperature becomes important. Details matter. During my process reviews, I have seen small changes in a rib or ejector position reduce distortion and visible marks.
Quality control should include material verification, first-article measurement, visual inspection, and checks for flash, porosity, and incomplete filling. Critical dimensions need recorded results, not verbal assurance. A reliable production team also tracks die wear and process parameters across batches. However, die casting is not ideal for every design. Very deep cavities, severe impact loads, or unstable requirements may demand another process. A common mistake is promising tight tolerances everywhere. That tradeoff matters. Good technical judgment sometimes means questioning the original design.