
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








China Top 10 Cluster Gears Manufacturers for Global Buyers?
China’s gear industry has become a practical sourcing option for automotive, agricultural, industrial, and power-transmission applications. This guide introduces ten Chinese manufacturers associated with Cluster Gears for global buyers seeking dependable production partners. The selection considers manufacturing experience, material control, machining capability, inspection systems, export service, and application knowledge.
A reliable supplier should explain its steel grades, forging or machining route, heat-treatment process, and final inspection method. Buyers should ask for measurable details, including tooth-profile accuracy, hardness ranges, runout limits, batch traceability, and available test reports. Factory audits can reveal important realities: clean grinding areas, calibrated instruments, controlled storage, and technicians who understand gear noise and load performance. Sample approval should come before large-volume purchasing.
The companies discussed may serve different requirements. One may excel at customized transmission parts, while another may offer stronger volume capacity or shorter development cycles. Pricing alone can mislead. Lead time, packaging, tooling ownership, communication, and after-sales support also affect total sourcing risk. No ranking is perfect. Supplier capabilities can change with equipment, management, or market conditions. Buyers should verify current certifications and request recent samples before making decisions. This article offers a professional starting point, not a substitute for engineering validation. Clear drawings, application data, and realistic tolerances will improve every supplier conversation. Small details matter.
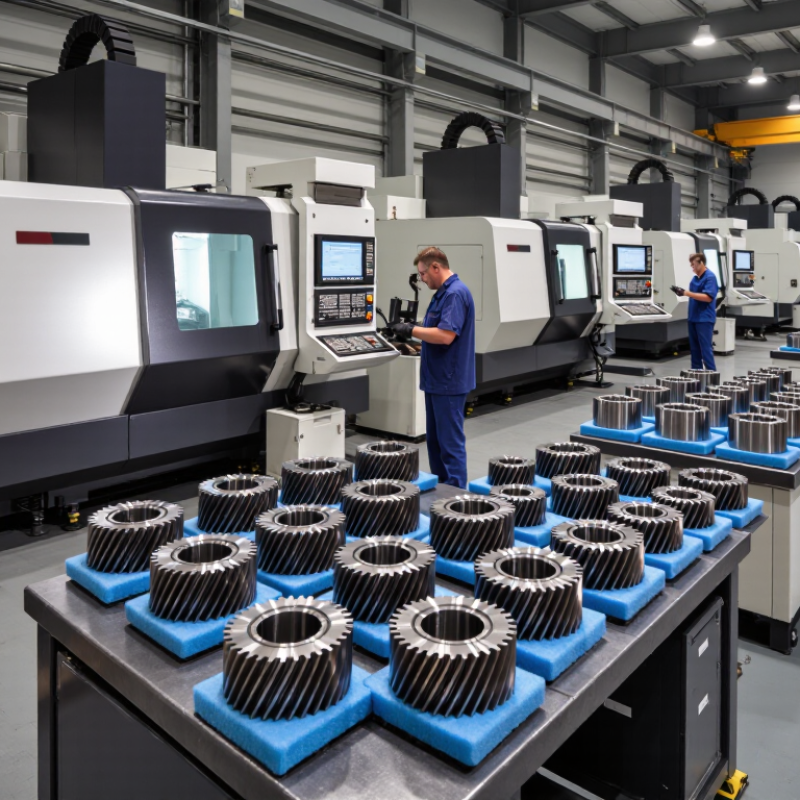
Table of Contents [Hide]
What Are Cluster Gears and Why Do Global Buyers Choose Chinese Suppliers?
China Top 10 Cluster Gears Manufacturers for Global Buyers
Cluster gears are grouped gears mounted on one shaft, transferring torque through several ratios. They appear in manual transmissions, reducers, agricultural equipment, and industrial machines. Their compact layout can deliver useful torque without demanding excessive installation space. That matters.
According to Grand View Research’s 2024 industrial gear analysis, the global industrial gear market was valued at more than USD 26 billion in 2023. MarketsandMarkets also forecasts steady growth through 2030, supported by automation, transport, and energy projects. These figures explain why global buyers examine Chinese suppliers closely. China offers broad machining capacity, competitive labor costs, and mature heat-treatment networks. Many factories can produce helical, spur, and synchronizer-related cluster gear components in medium or high volumes.
Price alone is a weak filter. Buyers should request material certificates, hardness records, tooth-contact reports, runout data, and load-test results. ISO 6336 calculations can help verify bending and contact strength before production. Supplier audits should also review traceability, inspection equipment, and corrective-action records. Chinese manufacturers often support customized modules, short trial batches, and export packaging. Yet quality consistency can differ between factories. A lower quotation may hide weaker steel control or insufficient final inspection. I would not accept a polished sample as proof of stable production. The better shortlist compares measured performance, delivery history, engineering communication, and documented process control.