
- High-Performance Doors
-
- Applications
-
-
-
- Clean Room
Stainless steel or composite materials help maintain clean rooms.
-
-
- Coolers
Quick opening speeds & tight seals for temperature control.
-
-
- Parking
Improve security & traffic flow and enhance architectural style.
-
-
- Hurricane Zone
Withstand winds up to 175 mph and comply with the Florida Building Code.
-
-
-
-
- USDA / FDA / cGMP
Increase productivity & address stringent USDA, FDA & cGMP requirements.
-
-
- Freezers
High-speed & perimeter seals minimize the air exchange between areas.
-
-
- Security
High speed & durability ensure secure access.
-
-
- Ventilation
Perforated or screen door panels allow improved air circulation.
-
-
-
-
- Fire Station Emergency Response
When time is of the essence, high speed and reliability are crucial.
-
-
- Warehousing
Fast cycle times and secure seals keep environments separated.
-
-
- Loading Dock
Rugged design & secure seal for oversized openings.
-
-
- Large Openings
Break-away functionality with rugged design seals oversized openings.
-
-
-
-
- Heavy Equipment
Withstands challenges of heavy equipment and fleet truck/car wash environments.
-
-
- Self-Storage
Fast opening speeds and reliable, durable construction keep facilities secure and protected.
-
-
- Industries
-
-
-
- Automotive Dealerships
Reduce energy costs, increase productivity and comfort and enhance customer perception.
-
-
- Cold Storage & Processing
Increase productivity and operational efficiency while reducing energy and maintenance costs.
-
-
- Parking
We offer solutions for Apartment / Condo & Loft, Standalone Parking Facilities and Office Buildings
-
-
-
-
- Food & Beverage
Doors specifically engineered for USDA/FDA and cGMP environments, and assured compliance for uncompromising performance.
-
-
- Mfg/Dist/Warehousing
A complete product line allows facilities to increase efficiency and safety and reduce maintenance and energy costs.
-
-
- Government
Ensure effective security and environmental controls are maintained for critical government operations.
-
-
-
-
- Transit
Keep operations running smoothly and efficient while reducing energy and maintenance costs.
-
-
- Pharma, Nutraceutical & Biotech
Doors that offer quick, secure access, environmental control and reliability for life science facilities.
-
-
- Support Resources
- Parts
- Contact Us
- Blog/News
- Why Rytec
- Sales Rep Locator
- Careers
- Dealers
- Architectural Resources








Top PVC Shoe Mould Manufacturers for Global Buyers
Choosing reliable Pvc Shoe Mould manufacturers requires more than comparing prices and product photos. Global buyers need suppliers that understand footwear production, export coordination, material behavior, and consistent mould performance. A strong manufacturer should explain its design process clearly, from 3D file review to CNC machining, trial sampling, and final inspection.
Experience becomes visible in practical details. Accurate mould dimensions help maintain stable shoe sizes across production batches. Suitable steel or aluminum selection affects durability, weight, and machining costs. Cooling channels, venting, surface finishing, and parting lines also influence mould quality. These details may seem small. They are not.
This guide introduces leading Pvc Shoe Mould manufacturers serving international buyers. It considers technical capability, factory equipment, quality control, communication, customization, packaging, and delivery reliability. Buyers should also examine sample approval procedures, replacement policies, and previous export experience. A polished website is not enough. Factory evidence matters more.
No supplier is perfect. Even experienced manufacturers may face delays when designs change late or samples require repeated adjustment. That risk deserves honest discussion, not exaggerated promises. Reliable companies usually provide measurable specifications, inspection records, realistic lead times, and responsive technical support. They also help buyers identify problems before mass production begins.
The following overview is designed to support careful supplier comparison. It does not treat low pricing as automatic value. Instead, it examines how each manufacturer balances precision, service, production capacity, and long-term dependability. For global footwear brands, the best choice is often the partner that communicates clearly and solves difficult mould problems before they become expensive production issues.
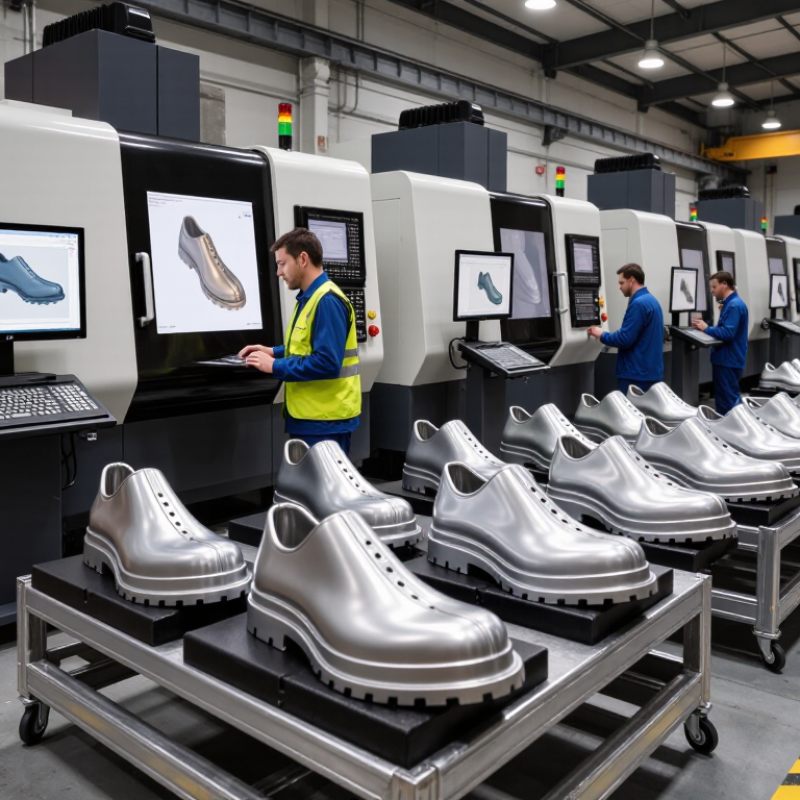
Table of Contents [Hide]
PVC Shoe Moulds: Types, Uses, and Key Manufacturing Standards
PVC shoe moulds shape soles, uppers, heels, and lightweight sandals through injection or compression processes. Each mould type serves a different production goal. Single-cavity moulds suit samples and small orders, while multi-cavity moulds improve output for established lines. Rotational designs can reduce material stress, but they may require longer cycle times.
In practical production, mould steel, surface finish, and cooling channels directly affect shoe quality. A polished cavity can create cleaner sole textures and simplify release. Balanced cooling helps prevent warping around the heel and toe. Venting is equally important. Poor venting may leave burn marks, trapped air, or incomplete details. Small defects become expensive when thousands of pairs are produced.
Reliable manufacturers should control dimensional tolerances, hardness, machining accuracy, and repeated cycle performance. They should also document material specifications, inspection results, and maintenance procedures. PVC compounds need consistent flow, color stability, and safe handling during processing. Buyers should request trial samples before approving mass production. A sample may look excellent, yet fail after repeated heating and cooling. That lesson is easy to miss.
Manufacturing should follow recognized quality systems and applicable product safety requirements in the target market. Clear drawings, revision records, and traceable inspections reduce misunderstandings between overseas buyers and mould makers. No mould is perfect. Even experienced teams may need to adjust gates, cooling paths, or texture depth after testing. That is normal engineering, not necessarily poor workmanship.